During production process, we may meet annoying issues:
A PCB project had passed several checks:
- Schematics passed DRC
- Production files passed DFM
- and the PCB have had been successfully assembled through SMT.
— yet quality problems such as bridging, solder nodules, and poor wetting still occur during the wave soldering process, impacting yield and production efficiency severely.
The root cause is not from the parameters of wave soldering, but from no process review during the design phase.
This article focuses on four design aspects which are frequently overlooked, with clear and quantifiable standards:
– Configuration of test points and solder pads
– Balance of thermal capacity
– Large copper foil areas
– Trace routing
1 | Test points placement:
Keep them “sufficiently clearance and isolated” from components
Test points must be placed separately from component pads, with a narrow trace, providing both electrical connection and physical isolation between them.
Quantifiable requirements are very specific:
◆ Passive components: Separate the test point from the component solder pad, by using a narrow trace with width 0.25mm;
◆ Active component: Separate by using a narrow trace with width 0.2mm, and the minimum spacing should exceed 0.4mm;
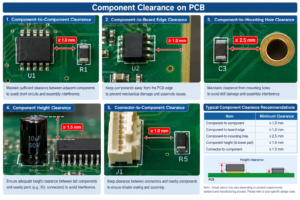
◆ The minimum clearance between the test point and the component body or pad must be at least 1.0mm;
◆ The distance to the center of any connector through-hole (DIP axial leads or cylindrical plug-in components) should exceed 2.5mm.
Mechanical stress will be generated during probe testing and test points are not directly transmitted to the component solder joints, thereby preventing the testing process from damaging the completed solder joints.
[Professional Insight]
Regarding to ICT(bed-of-nails testing), there are two additional practices for the industry:
1. Diameter of test point should not less than 0.8mm, and for high-requirement PCBs, points should be laid out on a 2.54mm grid;
2. Test points should be placed on the solder side, to avoid competing for space and conflict with high-density component areas.
If a test point also serves as a solder pad, repeated contact by flying probes can cause oxidation and damage to the pads, potentially creating invisible quality risks for future.
2 | Thermal analysis
It is required once PCBA design is completed.
This requires to analyzing the thermal capacity of the PCBA assembly and the impact of that capacity on each solder joint.
The essence of wave soldering lies in heating the soldering zone to the wetting temperature — a key step in the entire process.
Therefore, the design should avoid significant heat absorption in areas, which near to solder joints and ensure it as much as possible: every soldering zone on the PCB should absorbs heat equally, or nearly equal amount of heat during the wave soldering process.
Thermal capacity imbalances have negative influences on 2 directions:
◆ Areas with low thermal capacity:
Excessive heat supply → Overheating, potentially causing pad damage or copper foil delamination;
◆ Areas with high thermal capacity:
Insufficient heat supply → Low temperature, preventing proper wetting of solder joints → resulting in cold solder joints or “dry” (non-bonded) joints.
Typical scenarios of thermal capacity imbalance:
– Solder joints near large copper foil or ground plane areas, heating up slowly;
– Thick, multi-layer boards with high overall thermal capacity and solder joints near bulky components (such as transformers and electrolytic capacitors) having their heat “siphoned off.”
While layout optimization can be complemented by balancing preheat temperatures, the prerequisite is identifying “high thermal capacity zones” during the design phase — which is the value of thermal analysis.
3 | Large copper foil areas:
Improper handling can lead to solder nodules
Large copper foil areas are highly prone to forming solder nodules (localized solder accumulation) during wave soldering.
It occurs because molten solder spreads across the large copper surface but fails to retract smoothly, accumulating into nodule-like defects upon cooling.
Resolving strategies:
Divide large conductor areas into smaller traces or smaller sections, by using a grid pattern or “windowing” (openings in the copper).
Ideally, the narrow window strips should be oriented at a 45-degree angle relative to the board edge.
[Engineering Insight]
Large areas of copper foil have two adverse effects:
1. High heat capacity: They absorb heat from surrounding solder joints, leading to poor wetting;
2. Uncontrolled solder spreading: Solder tends to spread randomly, forming bulbous accumulations (solder blobs).
A 45° diagonal aperture pattern is the optimal solution.
The resulting narrow copper strips provide channels for solder retraction;
furthermore, the diagonal layout promotes more uniform heat dissipation and better mechanical stress distribution, than an orthogonal grid, preventing stress from propagating along the straight lines and causing cracking.
4 | Traces:
Prioritize rounded corners, avoid to use sharp or acute angles.
Trace geometry impacts PCB electrical performance significantly, and is a key factor influencing wave soldering defects (such as bridging, icicles/peaks, and solder blobs).
Key characteristics include trace shape, trace width, and trace spacing.
Core requirements for trace shape:
– Ensure smooth, uniform lines with gradual transitions;
– Strictly avoid sharp turns involving right angles or acute angles.
Acute angles cause two types of issues during wave soldering:
◆ Mechanical aspect:
Acute angles generate additional stress, leading to copper foil fracture, lifting, or delamination, which creates soldering defects;
◆ Soldering aspect:
Stress concentration causes cracks at acute angles, impeding the flow of molten solder and leading to excessive accumulation that forms solder blobs.
– Using rounded corners for both inner and outer transitions, prevents stress concentration and facilitates solder flow, preventing solder accumulation;
– Ensuring that bends in traces feature a transition where the rounded corner meets a straight segment, also promotes liquid solder flow;
– Conversely, sharp-angled bends are prone to trace breakage and solder blobs;
[Professional Insight]
Beyond rounded corners, there are three additional guidelines, regarding to trace geometry for wave soldering:
1. Align trace paths as parallel to the direction of solder wave flow, it is possible to minimize solder bridging between traces;
2. Using “teardrop” transitions for traces connecting to pads, it could relieve drilling stress and improve solder flow;
3. Trace width and spacing must meet three requirements: current-carrying capacity, insulation voltage withstand, and prevention of wave-soldering bridges;
In areas with dense, fine-pitch traces, it is prefered to increase the number of routing layers, rather than densely packing along, parallel traces on the solder side.
Wave Soldering DFM Design Review Checklist
| Review Item | Quantitative Standard / Recommended Practice | Defects to Avoid |
|---|---|---|
| Test Points | Keep test points separate from soldering pads. Use a 0.25 mm / 0.20 mm narrow-neck separation where applicable. | Solder joint damage caused by test probe stress |
| Clearance | Maintain ≥ 1.0 mm clearance from components and > 2.5 mm from connector hole centers. | Short circuits, probe interference, and assembly interference |
| Thermal Balance | Ensure equal or nearly equal heat absorption across all soldering zones. | Localized overheating, uneven soldering, and poor wetting |
| Large Copper Areas | Divide large copper areas using thermal reliefs, meshes, or openings; orient narrow copper strips at approximately 45° to the board edge where appropriate. | Solder blobs, thermal imbalance, and uneven solder joints |
| Trace Geometry | Use smooth, uniform, rounded transitions. Avoid sharp 90° corners and acute-angle routing. | Solder bridging, solder icicles, and copper trace breakdown |